1. Conveyor Belt Systems
This drive is ideal for controlling motors in conveyor belt systems used for material handling in manufacturing and logistics. Its precise speed and torque control capabilities ensure smooth and efficient product movement.
Problem SolvedProvides efficient and reliable speed/torque control for conveyor motors, enabling smooth acceleration/deceleration and accurate positioning of goods. The integrated Safe Torque Off (STO) enhances operational safety by quickly stopping motor torque in emergency situations, preventing unintended movement of the conveyor.
Motor controlVariable speed driveTorque controlMaterial handlingSafe Torque Off (STO)380-480V
2. Industrial Pump Control
Suitable for variable speed control of pump motors in HVAC systems, water treatment plants, and other fluid handling applications, optimizing flow rates and achieving significant energy savings.
Problem SolvedEnables demand-driven flow regulation for pumps, reducing energy consumption compared to fixed-speed operation. The 7.5 kW power rating and 380-480V input are well-suited for industrial pump requirements, while the IP20 rating allows for secure installation within a protected control cabinet.
Variable Frequency Drive (VFD)Pump motor controlEnergy efficiencyFlow optimization380-480V7.5 kW
3. Industrial Ventilation Fan Control
Applicable for controlling fan motors in industrial ventilation and air handling units, allowing for adjustable airflow to maintain optimal environmental conditions and reduce energy usage.
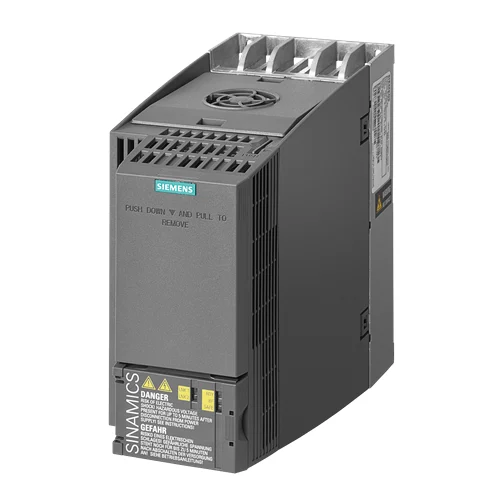
Problem SolvedOffers precise speed control for industrial fan motors, adapting ventilation rates to changing conditions and optimizing energy consumption. The compact form factor (196x100x203mm) facilitates integration into control panels even in space-constrained installations, and USS/Modbus RTU connectivity supports integration with building management systems.
HVAC systemsFan speed controlEnergy savingAir handling unitModbus RTUCompact design