1. Conveyor System Object Detection in Wet Environments
This sensor can reliably detect the presence and position of products on a conveyor belt in manufacturing and packaging facilities where exposure to water, coolants, or washdown procedures is common.
Problem SolvedEnsures consistent and accurate product tracking and counting in industrial settings, preventing errors due to sensor failure from moisture or contaminants, thanks to its IP67 rating and resistance to oils and coolants.
Object detectionConveyor systemsIP67Retroreflective3m sensing rangeOil/coolant resistance
2. Automated Material Handling in Cold Storage Facilities
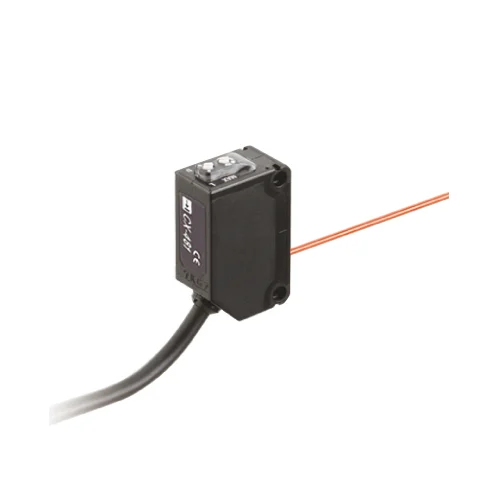
The CX-491-P-Z is suitable for detecting pallets or goods on automated guided vehicles (AGVs) or in cold storage warehouses, providing critical feedback for logistics and inventory management.
Problem SolvedOffers reliable detection in temperature-controlled environments, including freezers, due to its wide operating temperature range (-25°C to +55°C), ensuring continuous operation without performance degradation.
Automated Guided Vehicle (AGV)Pallet detectionCold storage-25°C operating temperature3m sensing rangePNP output
3. Machine Tool Presence Sensing with Enhanced Noise Immunity
Integrated into CNC machinery or other heavy industrial equipment, this sensor can monitor tool presence, workpiece positioning, or safety door closures, especially where high electrical noise is prevalent.
Problem SolvedProvides accurate and stable detection in electrically noisy industrial environments, preventing false triggers and enhancing safety and operational precision due to its high resistance to high-frequency noise and interference prevention function.
Machine toolPresence sensingElectrical noise resistance1ms response time12-24VDCShort-circuit protection