1. Automated Conveyor System Object Detection
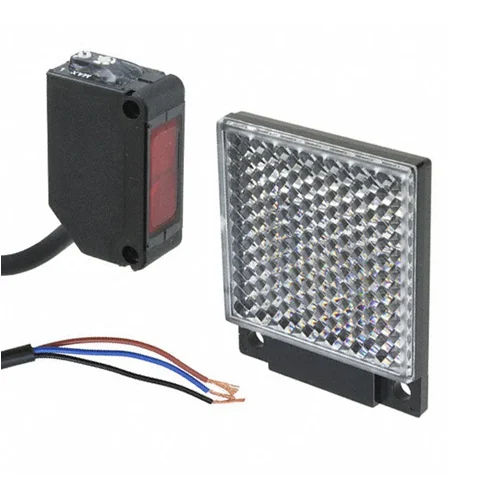
In manufacturing and logistics, the CX-491 can accurately detect the presence and position of various objects, including those with shiny or reflective surfaces, on conveyor belts. Its 3-meter sensing range and polarized filter prevent false detections from reflections, ensuring precise material handling.
Problem SolvedEnsures reliable object detection on conveyor systems, even for materials that are typically challenging for standard sensors due to their reflective properties, preventing jams and ensuring continuous flow.
Conveyor automationObject presence detectionPolarized retro-reflective3m sensing rangeNPN outputIndustrial automation
2. Packaging Line Product Counting
The sensor's fast 1ms response time and accurate detection of objects greater than Ø50mm make it ideal for high-speed counting of products in packaging applications. Its compact size allows for easy integration into existing machinery, and the IP67 rating ensures durability in packaging environments.
Problem SolvedProvides accurate and rapid product counting on high-speed packaging lines, contributing to efficient inventory management and quality control, even in environments with dust or splashes.
Product countingPackaging machineryHigh-speed detection1ms response timeIP67 protection
3. Machine Tool Area Monitoring in Harsh Environments
With its robust PBT housing, acrylic lens, and IP67 rating, the CX-491 can withstand the challenging conditions often found around machine tools, including exposure to coolants, oils, and metal dust. It can monitor safety zones or confirm part ejection, operating reliably in temperatures from -25°C to +55°C.
Problem SolvedOffers reliable sensing and safety zone monitoring near machine tools, resisting common industrial contaminants like coolants and dust, which would typically degrade less robust sensors.
Machine safetyHarsh environment sensingCoolant resistanceIP67Wide temperature rangeIndustrial monitoring